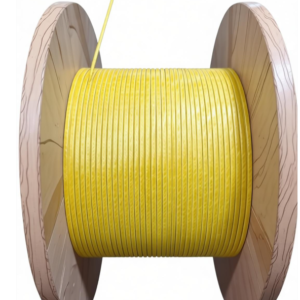
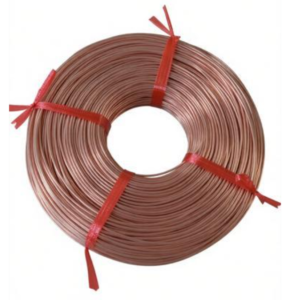
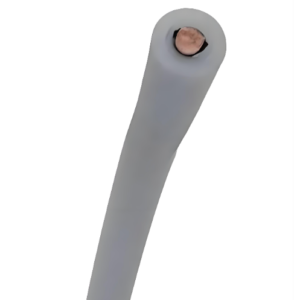
View more products about submersible pump winding wire+
The Wet Wound Stator: Direct Water Contact
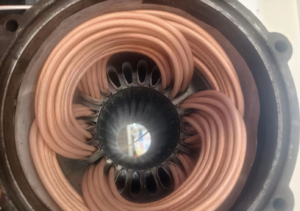
Understanding how PE/PA winding wire is used in submersible pump manufacturing requires understanding the wet wound stator design. In a wet wound stator, the copper wires of the stator winding are in direct contact with the liquid inside the motor . This is fundamentally different from potted or canned stator designs, where a protective can separates the winding from the surrounding fluid.
The wet wound approach offers distinct advantages. The winding is accessible, making the motor rewindable in case of electrical failure. The construction is simpler and more economical. However, these benefits come with a critical requirement: the winding wire itself must provide the entire insulation barrier against water ingress. The PE/PA construction was developed specifically to meet this requirement. Research published through the U.S. Department of Energy’s OSTI database, analyzing ten years of test data from 560 series-produced water-filled submersible motors, confirmed that PE/PA-type insulated windings (designated PEVVP and PVDP in that study) consistently satisfied insulation resistance requirements .
Wire Selection and Incoming Inspection
The manufacturing process begins with wire selection. For wet type submersible motors, PE/PA insulated wire is specified when the motor must operate at water temperatures up to 90°C, while PVC insulated wire suffices for applications limited to 70°C . The PE2 (cross-linked polyethylene) insulation offers higher thermal resistance than standard PVC, with the cross-linked molecular structure preventing the insulation from softening or deforming under thermal stress.
Incoming wire undergoes rigorous inspection before entering production. Dimensional verification confirms the conductor diameter within tolerances specified by JB/T4014, typically ±0.011 mm for 1.06 mm conductors . The insulation thickness must meet minimum requirements, with the thinnest point caused by eccentricity not less than 80% of the nominal thickness . The insulation surface is examined for bubbles, impurities, and mechanical damage. Insulation resistance testing verifies the dielectric integrity of the wire before it is wound into the stator.
Stator Winding Process
The winding process for submersible wet type motors presents unique challenges that distinguish it from conventional motor manufacturing. Academic research published in IEEE Xplore on manufacturing techniques for electric motor coils emphasizes that wire tension during winding is critical—improper tension leads to insulation damage, reduced fill factor, and compromised motor reliability . For submersible motors, these concerns are amplified because any damage to the insulation creates a direct path for water to reach the copper conductor.
The stator lamination stack is prepared with insulated slots, and the PE/PA wire is wound into the slots using automated winding machines. The winding pattern depends on the motor design: single-phase motors for smaller pumps use concentrated windings, while three-phase motors for larger units employ distributed windings. Throughout the winding operation, the PA sheath protects the underlying PE insulation from abrasion against slot edges and adjacent wire turns. The polyamide material‘s low friction surface allows the wire to slide easily through winding equipment and into the slots without snagging or scratching .
For submersible motors, a critical consideration is the end turn configuration. Patent literature on electric submersible pump manufacturing describes how form-wound coils can be preformed and inserted into the stator, rather than winding the wire directly into the slots . This approach reduces the risk of insulation damage because the wire is bent once during coil formation rather than being repeatedly threaded through slots. The formed coil method also permits better control over the wire tension and layering, leading to higher slot fill factors and improved thermal performance .
Insulation System Integration
Once the winding is complete, the stator undergoes further processing to complete the insulation system. For wet wound stators, the insulation relies primarily on the wire’s own PE/PA coating rather than varnish impregnation. Research notes that varnish is considered unsuitable for submersible motors facing hydrolysis from moisture ingress . The PE/PA insulation must therefore provide complete protection without the supplementary barrier that varnish would provide in conventional motors.
Some manufacturers apply additional protective coatings or encapsulation to the wound stator for enhanced water resistance. However, the fundamental insulation function remains with the wire itself. This is why the quality of the PE/PA winding wire is the single most important factor determining the service life of a wet type submersible motor.
Final Assembly and Testing
After winding, the stator is assembled into the motor housing with the rotor, bearings, and mechanical seals. The motor cavity is filled with a water-based mixture, typically containing glycol and water with a small percentage of non-toxic antifreeze . This fluid serves both cooling and lubrication functions, circulating through the motor to dissipate heat from the windings and lubricate the bearings.
Final testing verifies the completed motor‘s electrical integrity. Insulation resistance testing between the winding and ground confirms that the PE/PA insulation has not been damaged during assembly. High-voltage withstand testing applies elevated voltage to verify dielectric strength. For wet type motors, the test voltage is typically determined by the motor’s rated voltage, with test levels specified in applicable standards. Motors that pass these tests demonstrate that the PE/PA winding wire has maintained its insulating properties through the entire manufacturing process.
Applications and Market Position
China PE/PA submersible winding wire serves a global market for submersible pump motors. Applications range from agricultural irrigation and municipal water supply to mining dewatering and industrial process water management. For each application, the fundamental requirement is the same: reliable electrical insulation in a continuously submerged environment.
The cost advantage of China PE/PA winding wire does not come at the expense of quality. Manufacturers produce to JB/T4014 standards, which specify varieties, specifications, technical requirements, and inspection standards . The wire is available in conductor diameters from 0.6 mm to 4.0 mm, accommodating motor power ratings from small domestic pumps to large industrial units. For higher temperature applications, XLPE/PA wire extends the operating range to 90°C .
Technical Standards and References
China PE/PA submersible winding wire is manufactured in accordance with JB/T 4014 technical standards, which standardize varieties, specifications, technical requirements, and inspection standards for water-resistant winding wires . The rated working voltage is 450/750V, with design parameters specifying operation in water with pH value of 6.5 to 8.5 and water pressure below 10 kgf/cm² .
For international customers, the relevant Indian standard is IS 8783 (Part 4/Sec 1): 1995, which specifies requirements for PVC insulated winding wires for submersible pump motors . Academic research on motor coil manufacturing techniques is available through IEEE Xplore, providing authoritative guidance on wire tension, fill factor optimization, and insulation selection

Reviews
There are no reviews yet.